
Laser cutting of stainless and steel sheet in Bình Dương
LASER Tuấn Thịnh laser-cuts stainless, steel and aluminium to your drawing at its shop in Thủ Dầu Một, Bình Dương: up to 25 mm thick, parts to ±0.1 mm, quoted within 24 hours. Two fiber lasers (6 kW and 1.5 kW) on 3,000 × 1,500 mm beds, and automatic nesting keeps your material yield high and your unit price low.
Material, gas, edge
Gas choice decides the edge you get. Oxygen cuts thick steel fast with a light oxide film; nitrogen costs more and leaves stainless and aluminium clean enough to weld straight away.
Machine & tolerances
Kerf is compensated in CAM — holes and slots come out at drawn size, not drawn-minus-kerf.
By the hundred, or one of a kind
Parts nest tight into full sheets and run by the hundred — or send something no one has cut before: mandalas, Voronoi lattices, layered relief. If you can draw it, the laser can cut it. Swipe the gallery.
Draw it cuttable
Three rules cover 90% of rejected geometry. Break them knowingly and we'll flag it in the DFM notes rather than silently "fixing" your part.
Holes ≥ material thickness
Below 1×t the beam wanders and holes taper. Need a smaller hole? We pierce a pilot and you drill to final size.
Keep features off the edge
Holes closer than 1×t to an edge (or 2×t to each other) overheat and blow out — the web between melts.
Radius inner corners
A truly sharp inner corner doesn't exist — the beam has width. Draw R0.2+ and the corner comes out as designed.
Also free with cutting: etched part numbers and bend marks, so assemblies arrive self-explanatory. Just put them on a separate layer in your DXF.
What leaves the machine
Clean, weld-ready flat parts across electrical, automotive, signage, decorative, industrial, food-grade, HVAC and architectural work. Filter by industry, then open any photo full size and zoom in.
Dross-free underside on steel to 12 mm and stainless to 8 mm — no grinding before welding.
Deburred on request — edges broken by hand or through the deburring machine for handled parts.
Film-protected stainless stays filmed through cutting — brushed and mirror faces arrive unscratched.
Flat parts, guaranteed — we cut from levelled stock and re-level anything that moves on release.
Products made with this process
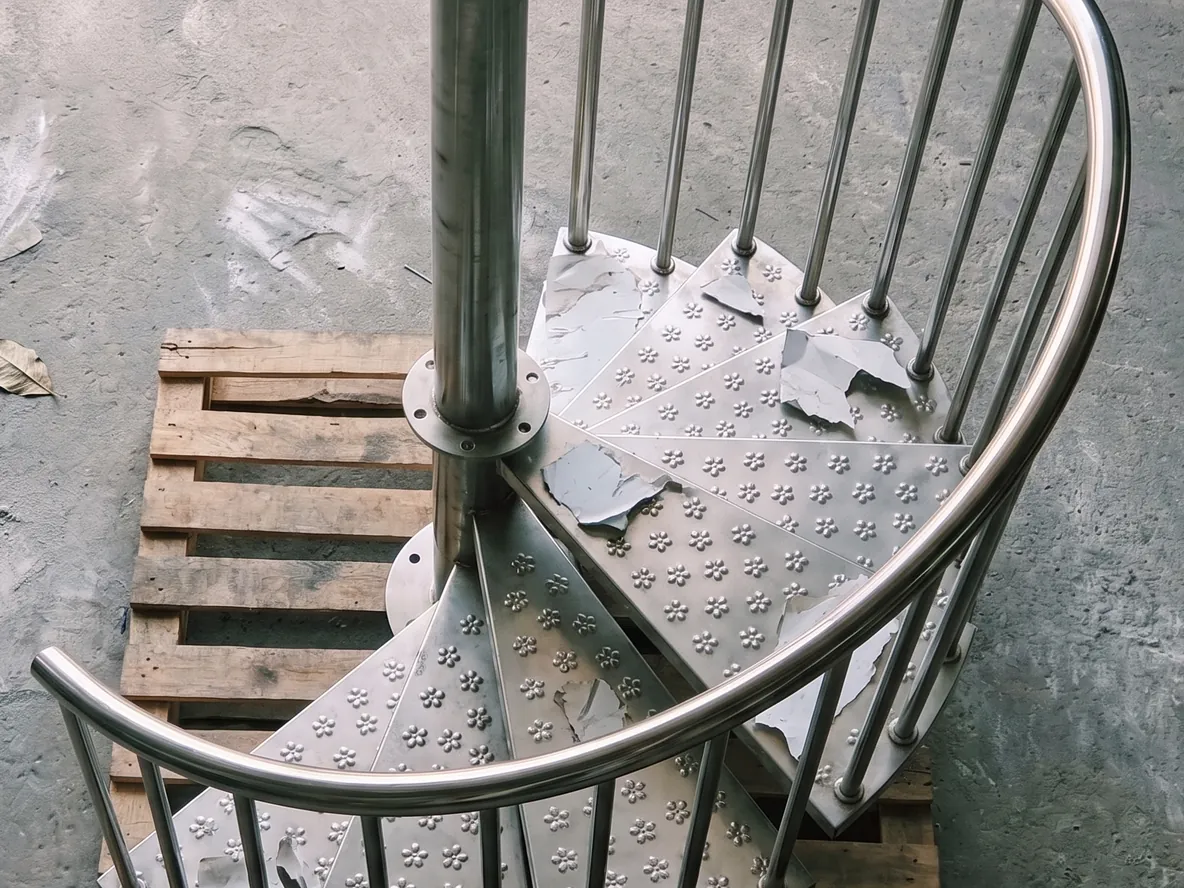
Made in our shop to your size, with reference prices.
Frequently asked questions
Send the drawing with your question — fastest way to a real answer.
01 Do you cut acrylic, wood, fabric or plastic?
No. We cut metal only: steel, stainless steel, aluminium, copper and brass, on fiber lasers. Acrylic, wood, fabric and plastic need a CO₂ laser, which we don't run.
02 How thick can you cut?
Steel, stainless and aluminium up to 25 mm, copper and brass up to 10 mm, on a 3,000 × 1,500 mm bed. Round tube from Ø15 to Ø114 mm runs on a separate tube laser.
03 Do you take small orders, even one piece?
Yes, from a single prototype to production runs. Small orders are nested on a shared sheet with other jobs to make the most of the material.
04 What files do you need for laser cutting?
DXF or DWG is best, and STEP, AI and PDF work too. No file yet? Send a hand sketch or a photo with dimensions and we can still quote. Quotes within 24 hours.
05 Do you deliver?
Yes, anywhere in Vietnam by freight or courier. The shop is in Thủ Dầu Một, now part of Ho Chi Minh City (formerly Bình Dương province).
06 Can you bend, weld and coat after cutting?
Yes. Cut parts are CNC-bent, tube-bent and TIG- or laser-welded in our own shop. Powder coating and galvanizing run at partner plants, and we handle the whole order.
07 What tolerance do you hold?
Laser-cut parts hold ±0.1 mm. Kerf width is compensated in the CAM software, so holes and slots come out at drawing size.
Nest it,cut it, ship it.
Send your DXF today — price and lead time back within 24 hours, DFM notes included.
