
From CAD file to coated part: the five stations a job travels
One file, one supplier, one purchase order. Follow a bracket from the drawing you email us to the finished part on your dock — the five stations it passes, and what happens at each.
The file lands
STATION · QUOTE DESKEvery job starts as a file in an inbox. A person opens it — not a portal — checks it against the same design rules the machine will care about later, drops it into a nest, and prices it. Most parts come back with a number the same day; a few come back with a red mark and a one-line fix.
Getting this station right is what makes the other four fast. A clean, complete file goes straight from inbox to nesting; a vague one bounces, and the clock you think is running hasn’t started.
Cut
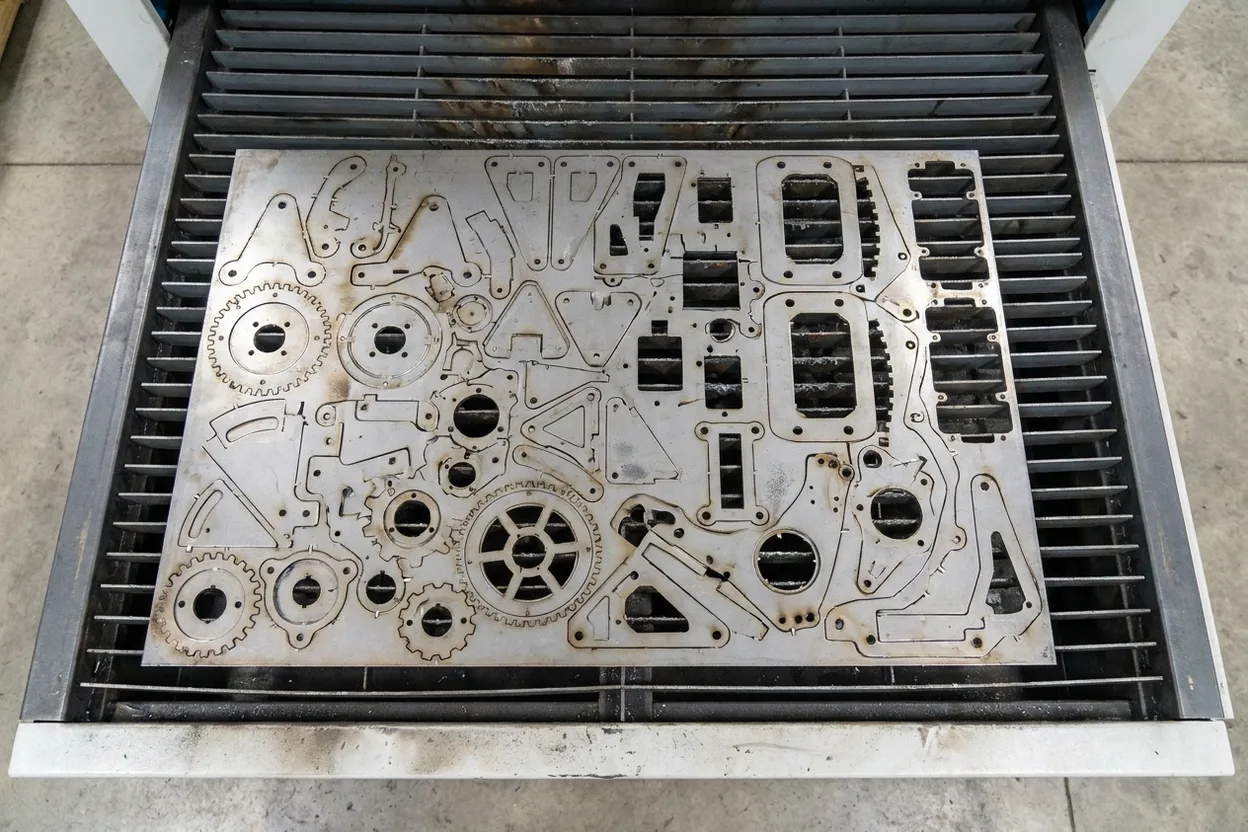
STATION · FIBER LASERFlat parts drop onto the fiber laser — 0.5 to 25 mm in steel, stainless and aluminium. Tube and profile go to the tube laser, which copes, mitres and marks weld lines in the same setup, so an assembly arrives at the weld bay ready to fit with no hole-saw and no jig.
Form
STATION · PRESS BRAKEFlat blanks become 3D on the press brake; tube is bent on the rotary-draw bender. Both fight the same enemy — the metal springs back a few degrees after the tool releases, so we measure it, predict it, and over-bend to land on your angle.
Join
STATION · WELD BAYFormed parts are jigged square, tacked, then welded — TIG for the clean and the thin, handheld laser for precision seams and heavier sections. Stainless gets back-purged so the root stays bright, and every weld is ground and dressed to the standard the job asked for.
A part is only as straight as the fixture it was welded in. We build the fixture first.NOTE TAG · TAPED TO THE NESTING PC
Finish & ship
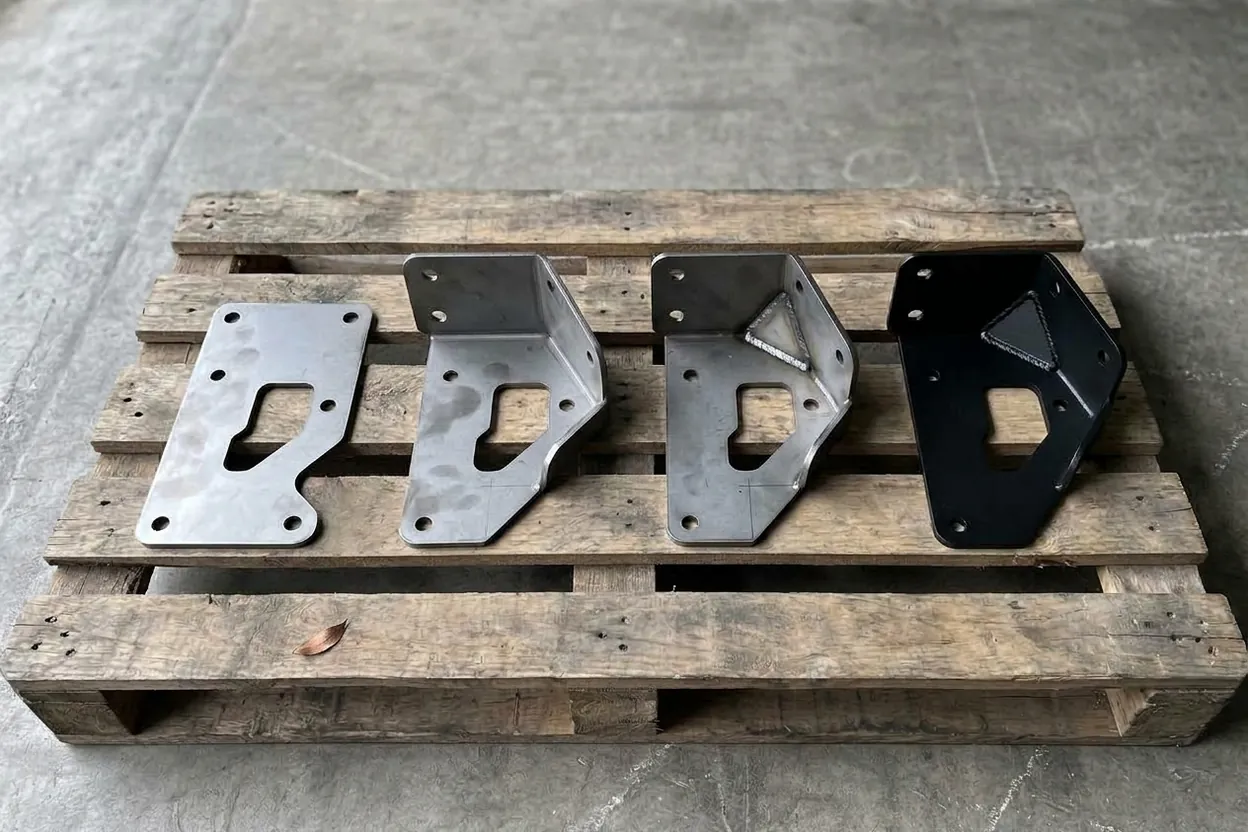
STATION · PARTNER POWDER LINELast stop: the surface. For this the parts leave our shop for the partner coating line we use, with the finish and colour we specify. Steel is blasted, stainless passivated, then parts hang through a 7-stage pretreatment and the powder booth — any RAL, matt to metallic — and cure hard in the oven. Threads and mating faces stay masked and bare. We handle the transport both ways, and the parts come back under the same order.
Then it’s checked against the drawing, its heat numbers logged, labelled and packed for transit. The same part you drew leaves the dock coated, inspected and ready to bolt in — off one purchase order.
- Key dimensions checked against the drawing Measured, not eyeballed — the ones you flagged plus the ones that stack up.
- Finish to spec, masking removed Right RAL and gloss; threads and earth points bare and clean.
- Heat numbers logged Traceable from stock rack to nest to your delivery note — 3.1 certs on request.
- Labelled and packed for transit Edges protected, quantities counted, marked to your part number.
Have a part to make? Start a job.
